The tier count that looked right on paper and lost a third of its facings
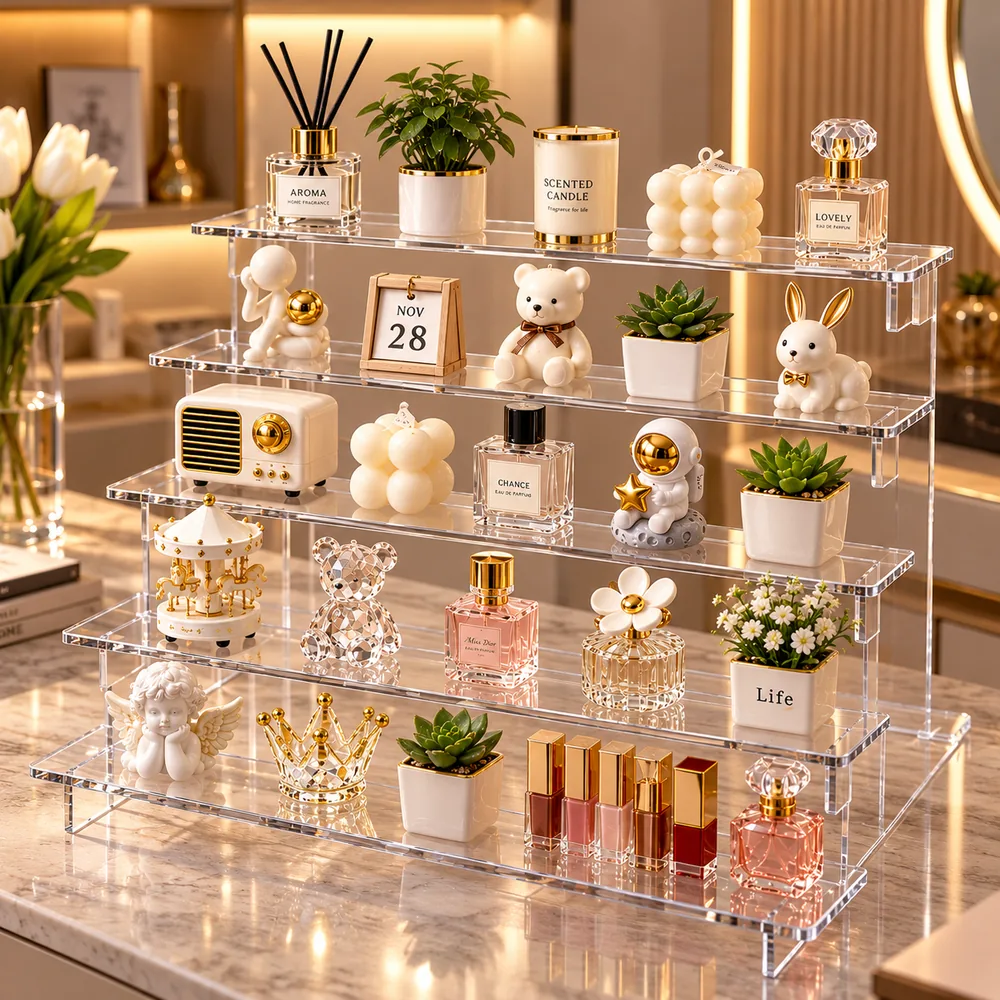
A tiered display is usually specified from a photograph of a similar unit. The photograph shows a shape, not a capacity, and the difference between the two is one measurement that is almost always left out.
Illustrative procurement scenario. This is not a customer case, and no outcome or performance figure is claimed.
The situation
A buyer needs a counter unit for a range of twelve SKUs in three pack widths. A supplier photograph shows a four-tier ladder that looks close to what is wanted, and the enquiry is written from that image: four tiers, about this size, same look.
The unit is made to the photograph. The packs arrive, the store fills it, and the front row cannot be loaded because the tier above sits too low for a hand to reach in. Two of the four tiers end up holding product at half depth. The unit shows fewer SKUs than the flat tray it replaced.
Where the specification actually failed
Nothing was wrong with the tier count. The failure was that tier spacing was copied from a unit designed for a different pack height, and no one had measured the removal path.
Three numbers decide a tiered display, and only one of them is a product dimension:
- The width of the widest pack, plus the clearance a hand needs to take it out
- The height of the tallest pack, which sets the clear gap between tiers
- The counter depth available, which sets how many tiers the unit can have before the back row becomes unreachable
How the decision should be made
Work from the cell outwards. Set the cell from the widest pack plus removal clearance, work out how many cells fit across the available width, then work out how many tiers fit in the available depth and height. The tier count is the last number produced, not the first one chosen.
If the answer comes back as three tiers instead of four, that is the honest result. A four-tier unit that cannot be loaded is not a four-tier unit.
What changes once the tier count is fixed
Tier count drives sheet size, the number of joints, the packed volume and the carton. Moving from four tiers to three is not a small edit to a drawing: it changes the sheet yield, the joint count and the freight per unit, so it is quoted as a new configuration rather than an adjustment.
That is also why the tier count should be settled before a sample is cut. A sample made to the wrong tier count confirms nothing except that the wrong unit can be manufactured.
Send this in the RFQ
- Pack width, height and depth for each product family, not just one sample SKU
- How many facings each SKU needs on the counter
- Counter depth and height available, and whether the shopper reaches from the front or the side
- Whether packs are removed by hand or read in place